Founded 2013 · Guangdong, China · LSR

From a drawing
to a production-ready silicone part

Zhongshan Runweikang Silicone Technology develops liquid silicone rubber (LSR) products, designs and builds the tooling, and molds the parts — under OEM, OBM and ODM programs. Thirteen years doing one thing — silicone products: the standard parts made precise, the difficult parts made stable.

Molding processLIM · Liquid Injection Molding
Signature processPPSU / PA / PC / PP / metal overmolding · volume proven
CleanroomClass 100,000 (ISO 8)
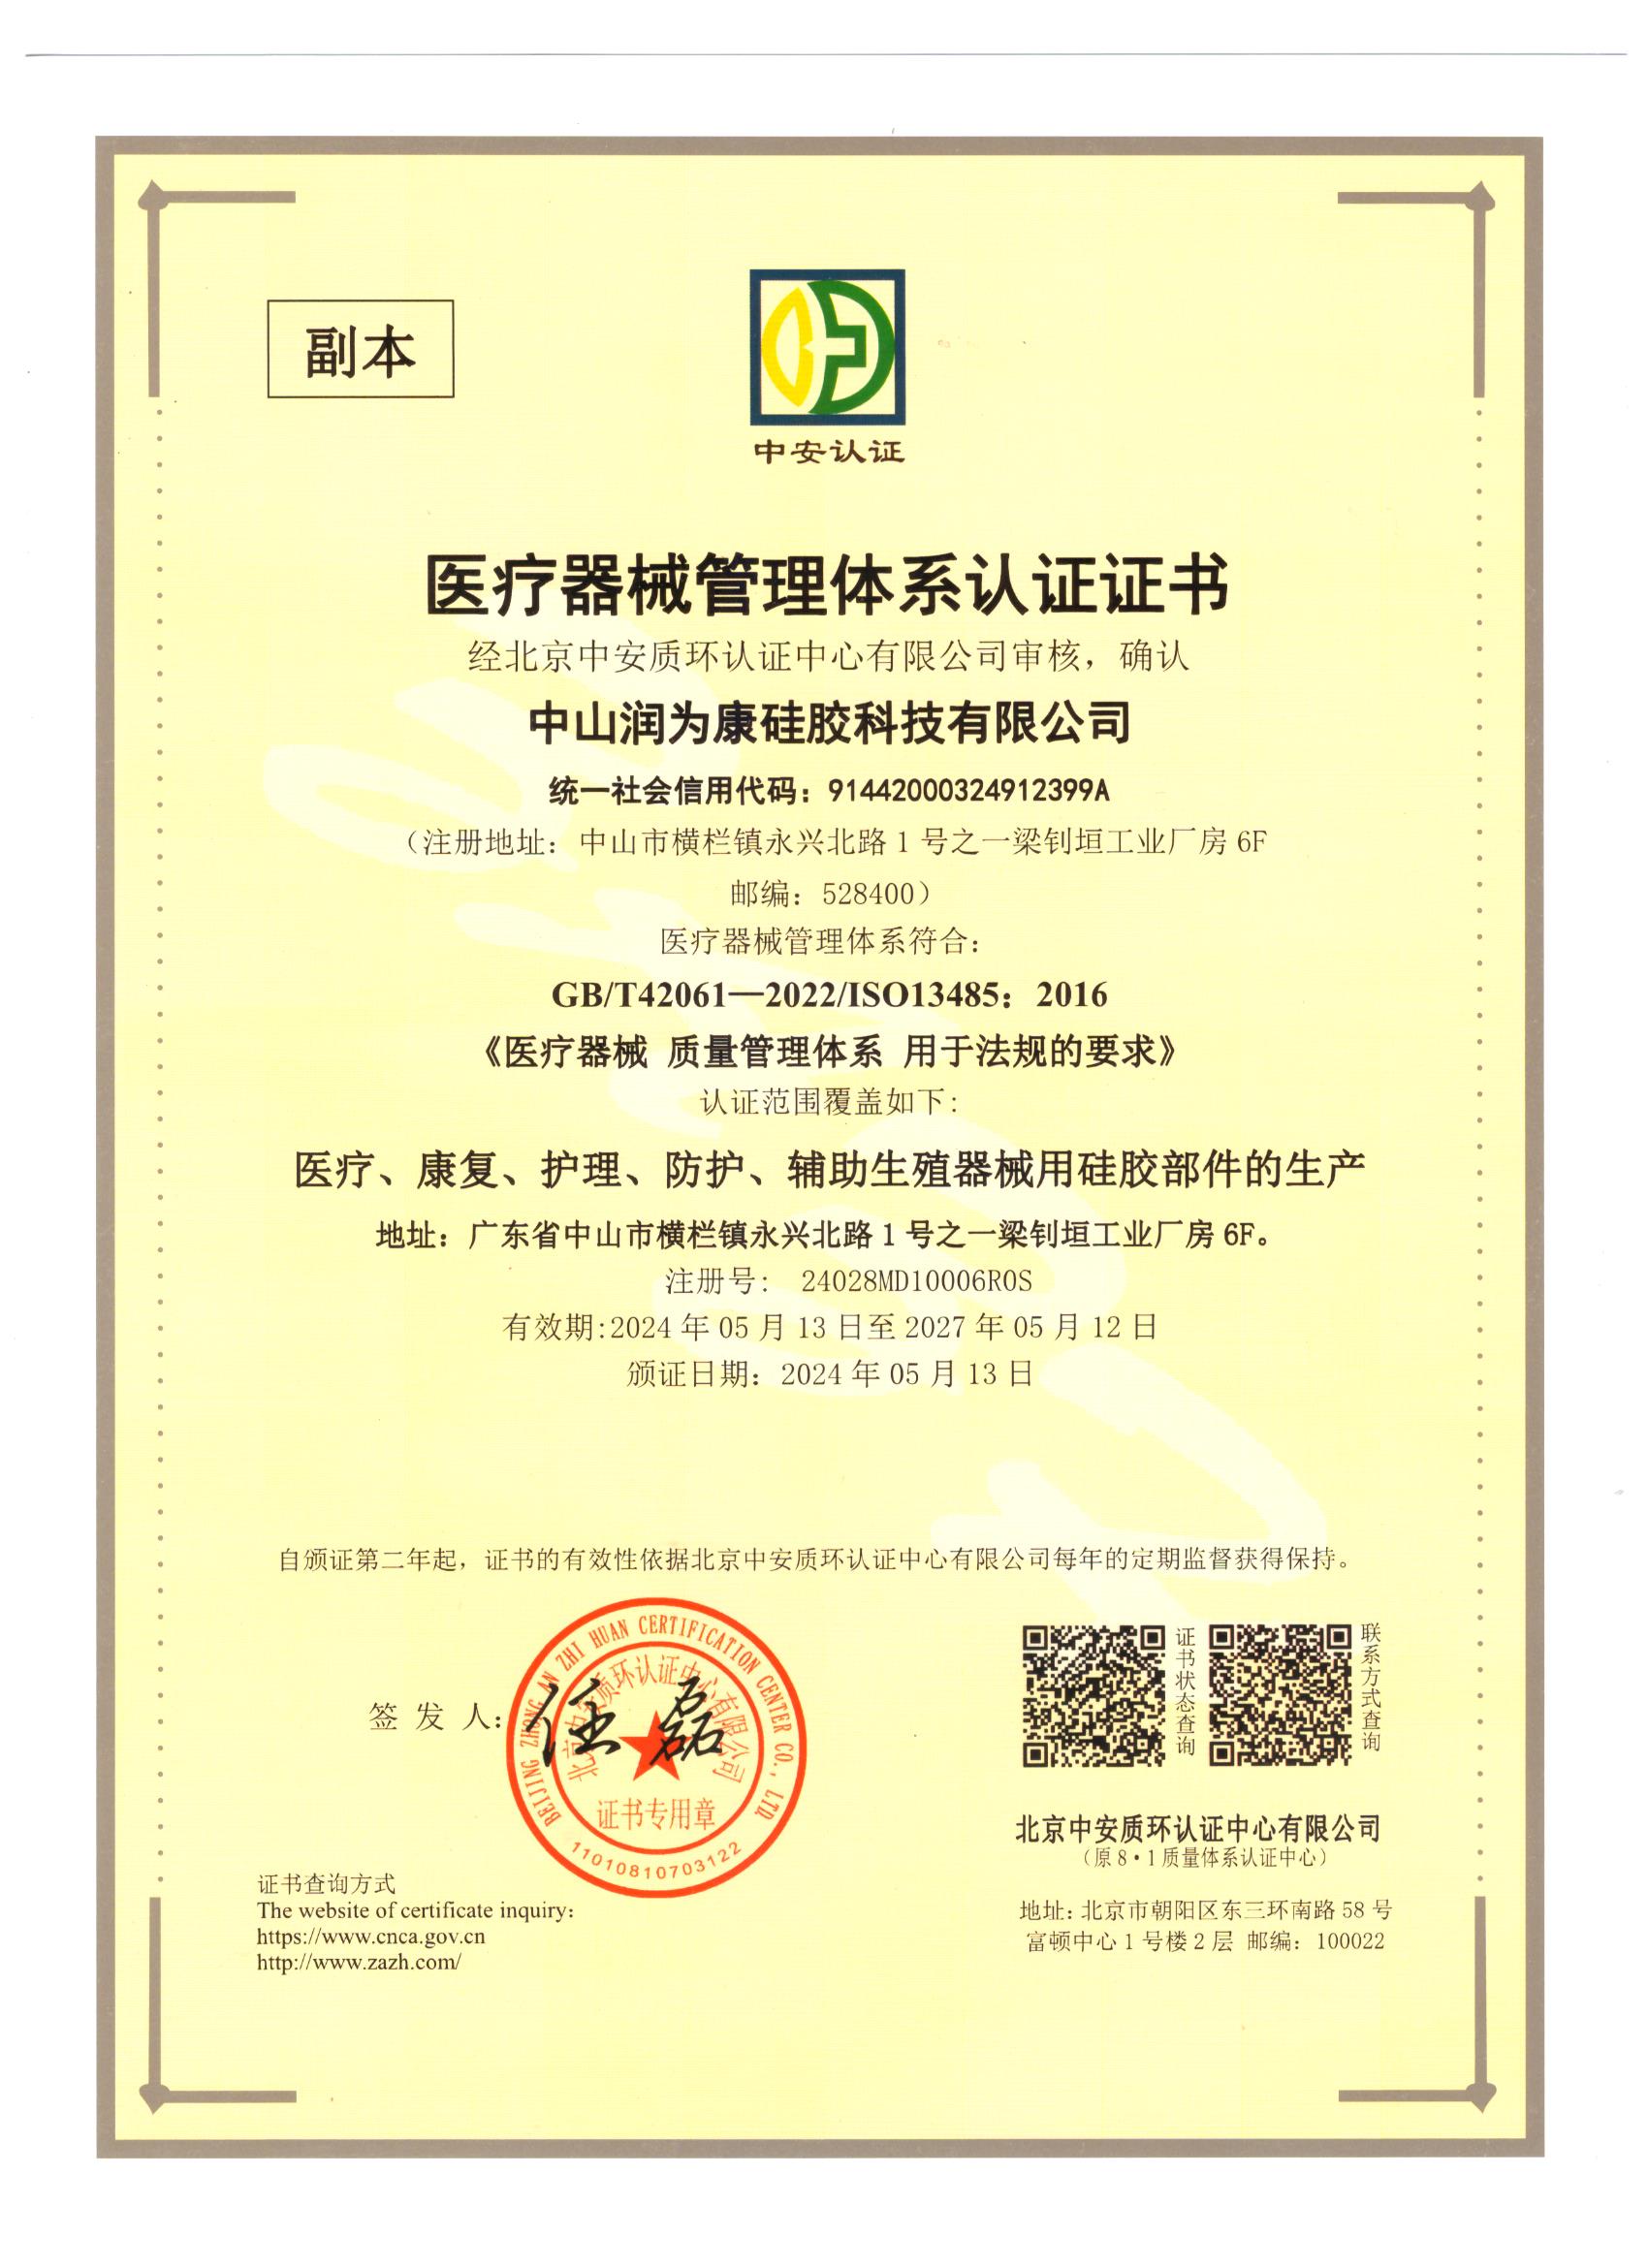
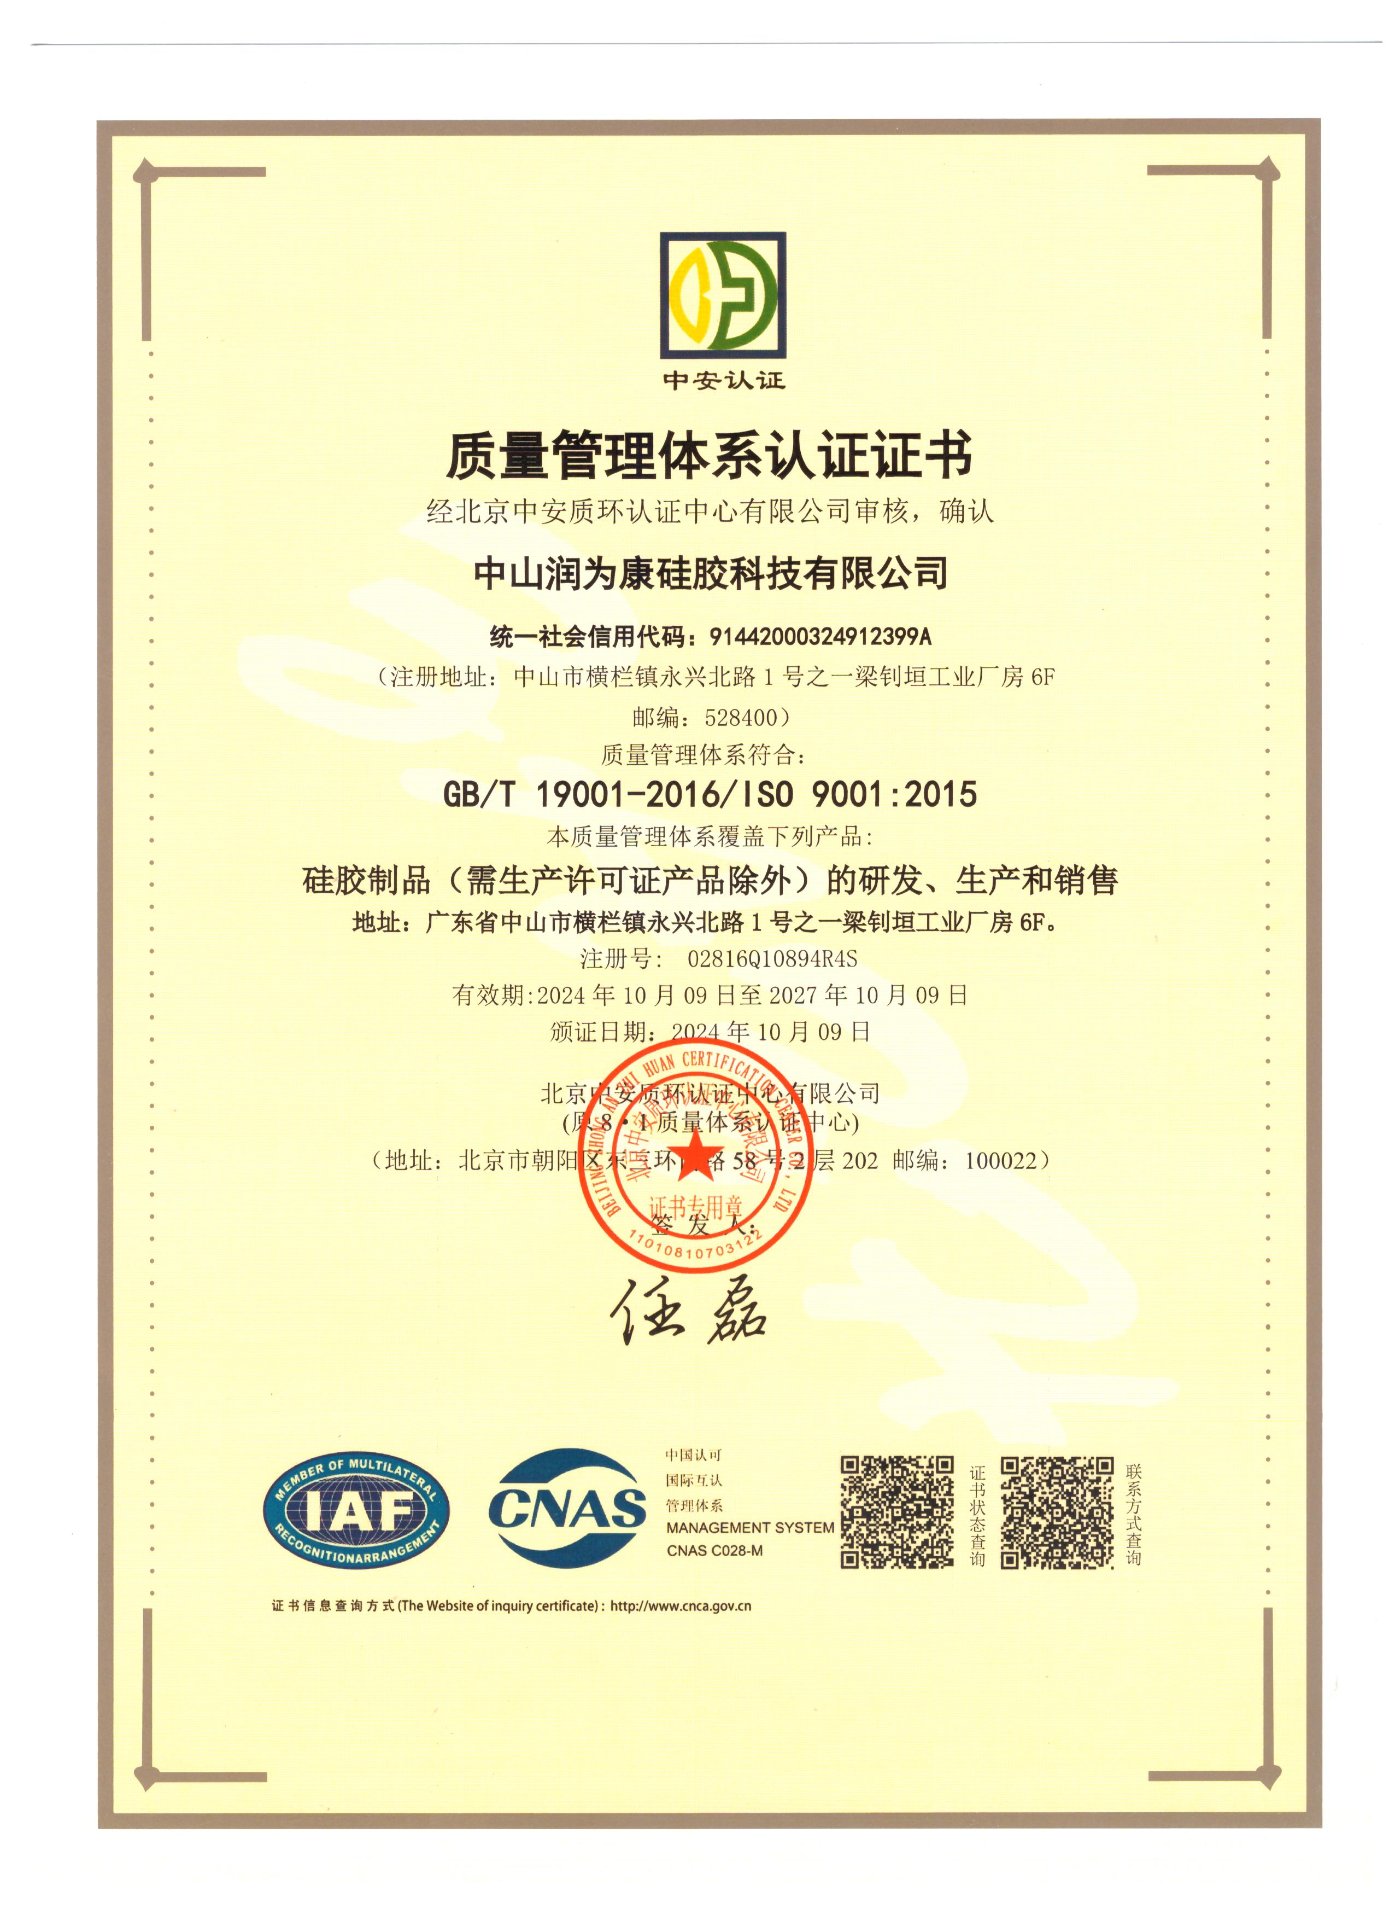
CertificationISO 9001 / ISO 13485
Business modelOEM / OBM / ODM
LocationHenglan, Zhongshan, Guangdong
13yrs
Focused on LSR
13units
Injection molding machines
30+
Patents filed
100K class
Cleanroom production
COMPANY PROFILE

A factory that does one thing: liquid silicone

U-WECAN Class 100,000 cleanroom and LSR injection moulding line

Zhongshan Runweikang Silicone Technology Co., Ltd. was founded in 2013 and is located in Henglan Town, Zhongshan, Guangdong. We develop liquid silicone products, design and build the molds, and manufacture and sell the molded parts — supported by a team of experienced technical and production staff.

The plant runs LIM (liquid injection molding) in a Class 100,000 cleanroom with dedicated laboratory and packing areas. The lab controls inspection data across the whole production chain: a 2.5D optical measuring system for dimensions, VOC testing for volatiles. Every batch carries traceable dimensional, cosmetic and outgassing records.

Over thirteen years we have built up a material library and a set of process windows for infant feeding, medical silicone components, overmolded structures, seals and precision optical parts. The point is not to make silicone parts. It is to make silicone parts repeatable.

Product quality as the baseline — it is written into our company profile, and into every production line we run.
MANUFACTURING

From “we can make it” to “we can make it the same way, every time”

We own the equipment, the cleanroom and the inspection line. That is what lets us commit to batch-to-batch consistency.

Class 100,000 cleanroom
Temperature- and humidity-controlled. Medical and infant products are molded, inspected and packed inside the clean zone.
13 LIM injection molding machines
120T and 140T presses in a mixed configuration, covering high-cavity small parts and mid-size parts with flexible scheduling.
In-house laboratory
2.5D optical measurement and VOC test equipment, so dimensions, appearance and volatiles stay traceable by batch.
Tooling built in-house
Solid and liquid silicone molds plus plastic molds. From DFM review to trial shots, all under one roof.
PRODUCTS

Six product lines

Compounds and process windows are managed per application: infant mouth-contact parts, medical devices, industrial seals, optical parts.

View products
Baby feeding line: silicone overmolded PP / PPSU bottles, teethers and sippy cups
01
Infant grade

Infant feeding products

Baby bottles, silicone bowls, training cups, teethers and nipples. Our strength is silicone-over-PP and over-PPSU bottle bonding: a 360° overmold separates the plastic from the contents, with leak-tight, drop-resistant structures — BPA-free, softness and rebound tuned to how a baby feeds.

Bottle overmoldingTeethersTraining cups
Medical silicone parts: seals, tubing connectors and respiratory components
02
Medical grade

Medical silicone components

Medical seals, catheter and respiratory parts — silicone components for medical, rehabilitation, nursing, protective and assisted-reproduction devices. Molded inside a Class 100,000 cleanroom under ISO 13485, batch traceable, compatible with common sterilization methods.

ISO 13485Catheter connectorsRespiratory masks
Close-up of PP-to-silicone bonding interface on an overmolded part
03
Overmolding Rare process

Silicone overmolded parts

PPSU, PA and PC overmolding are mature, high-volume processes for us, as is overmolding onto stainless steel and metal inserts. The hard part is bond strength, fatigue resistance and cosmetic consistency. PP + silicone is harder still — very few plants in China can hold it at volume, and it is our core process moat.

PP overmoldingPPSU overmoldingMetal overmolding
Silicone seals, wire harness grommets and O-rings
04
Sealing

Silicone seals

Metal-bonded seals, wiring-harness boots, O-rings and custom sealing geometries. Silicone's temperature range and aging resistance outlast general-purpose rubber outdoors, in engine bays and in humid environments; dimensional stability comes from tooling and cure parameters together.

Harness bootsO-ringsCustom profiles
Silicone lenses and optical-grade precision parts
05
Precision

Silicone lenses & precision parts

Silicone lenses, optical-grade precision parts and thin-wall components. 2.5D measurement and VOC testing keep dimensions and appearance traceable, batch after batch.

Silicone lensesThin-wall partsOptical grade
LSR moulds and cold-runner systems
06
Engineering

LSR tooling

Solid and liquid silicone molds, plus plastic molds. DFM analysis, tool build and trial runs run in sequence in-house, so design changes do not wait on an outside tool shop's schedule.

DFM analysisCold runnerMulti-cavity
PROCESS MOAT
The hard one: PP + silicone overmolding

PP is a low-surface-energy, non-polar semi-crystalline plastic. Chemically it has almost nothing in common with silicone — and the harder constraint is thermal: PP's heat deflection temperature (roughly 90–105°C) sits right under LSR's cure temperature (above 120°C), leaving only a narrow slot to work in. Plenty of plants can produce a sample; very few can hold it in volume, month after month — which is why customers bring their PP projects to us. PPSU, PA and PC overmolding, by contrast, have long been routine production here.

Mature at volume PPSU / PA / PC · stainless steel · metal inserts Rare at volume PP + silicone
18monthsFrom material screening to a frozen process recipe
DozensSubstrate–silicone combinations screened, one by one
70×5-minute boils with cooling in between, cycled
Why it fails
Low surface energy and no polarity, so silicone has nothing to grab. PP holds its shape only up to 90–105°C while LSR needs above 120°C to cure: too cool leaves it under-cured, hot enough creeps the substrate out of tolerance. The window is razor thin — and infant sterilization duty (100°C boiling water) sits right on that edge.
Three matches
The compound's hardness and shrinkage have to suit the PP, the substrate grade has to be locked, and the primer system has to be both compatible with the silicone and hydrolysis-resistant. Get any one wrong and the lot fails — usually after tens of boils, not on day one.
How we prove it
We do not ship on initial adhesion. Parts are cycled through 70 boils of 5 minutes plus cooling; no delamination, blistering or separation is the pass criterion. That is the number infant-product buyers actually care about.
From zero to a fixed recipe, this process took us 18 months: dozens of substrate–silicone combinations screened one by one, multiple rounds of process fitting and testing, repeated tooling and line trials — before the recipe could be frozen. The specific grades and primer system belong to our process file and are not published here; the criteria and the test method, we are glad to explain in full. If your product is stuck at the PP bonding step, send us the drawing or a sample and we will assess feasibility on the existing line.
INDUSTRIES

Four industries, four process recipes

Material requirements differ widely between these markets. We have built a dedicated compound library and process experience for each.

Mother & baby feeding
Bottles, silicone bowls, teethers, nipples and training cups with silicone-over-PP / PPSU bonding. Every mouth-contact material is traceable.
Medical devices
Medical seals, catheter and respiratory components, molded inside a Class 100,000 cleanroom under an ISO 13485 system.
Industrial & automotive
Metal-bonded seals and wiring-harness boots for automotive, machinery and outdoor equipment sealing and protection.
Consumer electronics
Electronic silicone parts, silicone lenses, dive masks and eyewear cases. Thin-wall precision molding with optical-grade clarity.
KNOWLEDGE HUB

LSR Academy

We write down what we have learned about materials, processing and part design. It saves engineers time — and it is how they find us.

All articles
CERTIFICATION

Two management systems

ISO 9001 covers development, production and sales of silicone parts across all product lines. ISO 13485 covers silicone components for medical devices.

ISO 13485 medical device quality management system certificate
ISO 13485:2016 Medical device QMS
GB/T 42061-2022 · valid to May 2027 · covers silicone components for medical, rehabilitation, nursing, protective and assisted-reproduction devices
ISO 9001 quality management system certificate
ISO 9001:2015 Quality management system
GB/T 19001-2016 · valid to October 2027 · covers development, production and sales of silicone parts
30+patents filed, covering mold structures, overmolding processes and molding equipment
Certificates and patents

Have an LSR project in motion? Send us the drawing

Share 2D / 3D files or a sample. Our engineers run a DFM review first, then come back with a prototyping and production plan — including difficult substrates such as PP and PPSU.

Send an inquiry